Pharmaceutical & Medical
Automation Solutions
MASK Control Systems designs and delivers automation solutions for pharmaceutical and medical device manufacturers across the UK and worldwide. Since 2013, we have engineered PLC control systems, control panels, and fully integrated automation solutions for clean-room and validated environments, where regulatory compliance and data integrity matter as much as performance.
Our team understands the standards, the documentation, and the validated-state discipline that define this sector, and we build every project around them.
Why Pharmaceutical & Medical Manufacturing Needs Specialized Automation
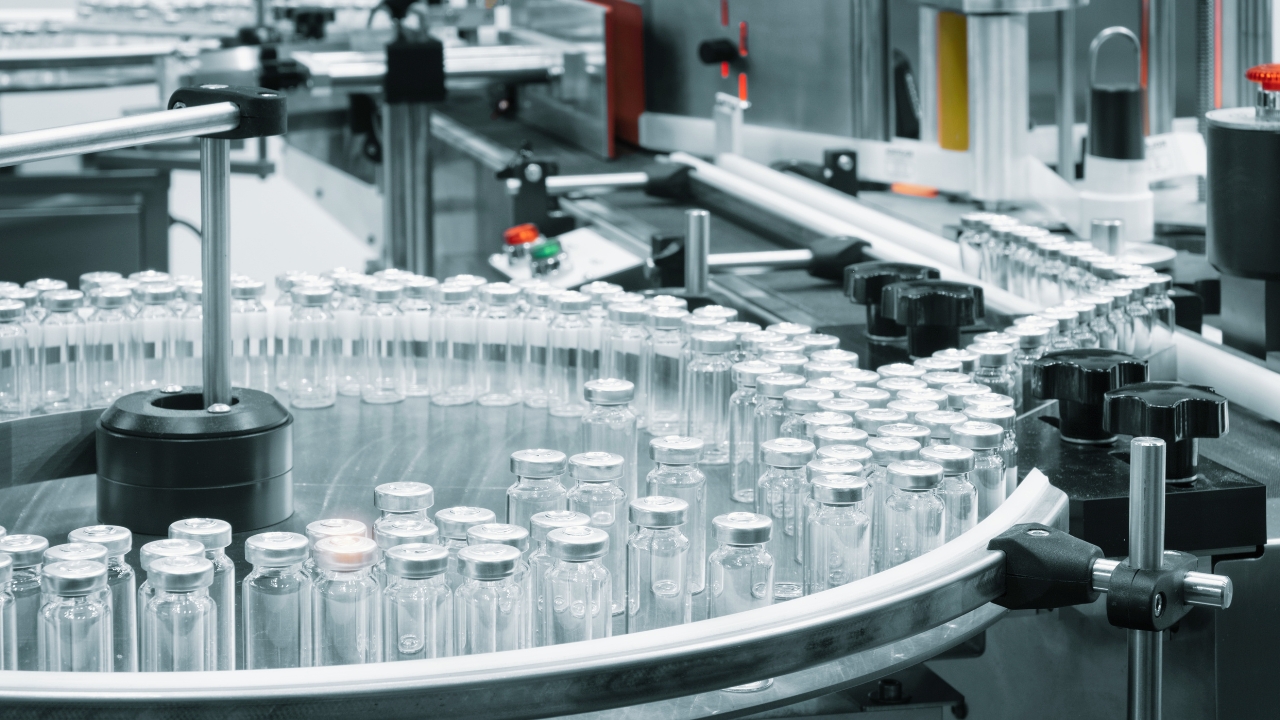
Pharmaceutical and medical device manufacturing operates under some of the strictest requirements of any industry. Automation systems in this sector cannot simply be dropped into a clean-room environment.
Airflow & Clean-Room Integrity
Airflow behavior, material flow, and contamination control need to shape the automation design from the earliest planning stage, or the clean-room's integrity is put at risk.
Preserving the Validated State
Once a facility is validated, every system change—whether a software update or a hardware modification—must preserve that validated state under strict change control.
Data Integrity & Audit Trails
Batch records and process data must be complete, traceable, and free of gaps. A single missing record can compromise an entire regulatory audit and hold up product releases.
Fill-Finish & Batch Sequencing
Batch release and fill-finish processes demand precise, repeatable sequencing, with zero room for variation between cycles. We design every system with these realities built in from day one.
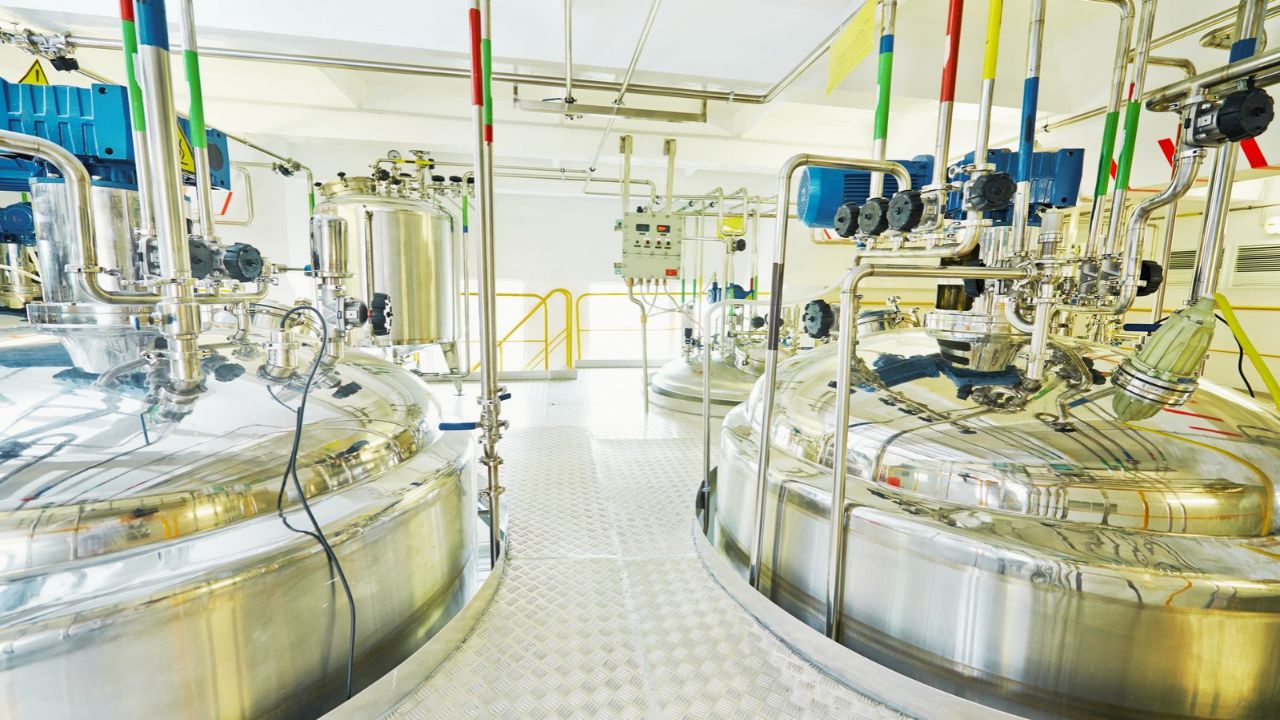
Supporting pharmaceutical manufacturers, vaccine laboratories, cell therapy clean-rooms, and medical device assembly lines across the UK with GAMP-compliant automation.
The UK Pharmaceutical & Medical
Manufacturing Landscape
Pharmaceutical and life sciences manufacturing is currently the fastest-growing segment of UK industrial automation, expanding at a compound annual growth rate of 13.77 percent. This growth is being driven by rising demand for clean-room automation, batch-release systems, and fill-finish processes, particularly across vaccine and cell therapy production.
This rapid growth has not been matched by an equivalent growth in specialized talent. Automation engineers with genuine validation and GAMP experience remain in short supply across the UK, and many pharmaceutical and medical device manufacturers struggle to recruit or retain that expertise in-house.
As a result, more manufacturers are turning to experienced outsourced partners like MASK Control Systems who already understand validated environments, rather than trying to build that capability from scratch internally.
Signs Your Facility Needs Pharmaceutical Automation Support
Several recurring signals tell us a pharmaceutical or medical device facility is ready for an automation review before issues affect your next regulatory inspection:
Manual Paper-Based Batch Records
Batch records are still tracked manually or on paper, slowing down regulatory audits and elevating human transcription error risks.
Validation Maintenance Challenges
Maintaining a validated state after minor equipment or software changes has become increasingly difficult, costly, and time-consuming.
Aging SCADA & Data Integrity Gaps
Legacy SCADA or PLC control systems can no longer support modern FDA 21 CFR Part 11 data integrity and electronic signature expectations.
Manual Environmental Logging
Critical clean-room environmental monitoring (temperature, differential pressure, humidity) still relies on vulnerable manual logbooks.
GAMP & Validation Skills Deficit
Your in-house engineering team lacks specialized GAMP 5 or formal computer system validation (CSV) experience for upcoming plant upgrades.
Audit Flags on Change History
Recent MHRA or FDA audits have flagged gaps in control system change control, traceability documentation, or software versioning.
Experiencing data integrity or validation bottlenecks?
An automation review is worth prioritizing before audit findings or batch deviations escalate.
Our Pharmaceutical & Medical
Automation Services
From clean-room control panels to 21 CFR Part 11 compliant SCADA and independent environmental monitoring, we engineer automation systems built around data integrity, repeatable precision, and qualification readiness.
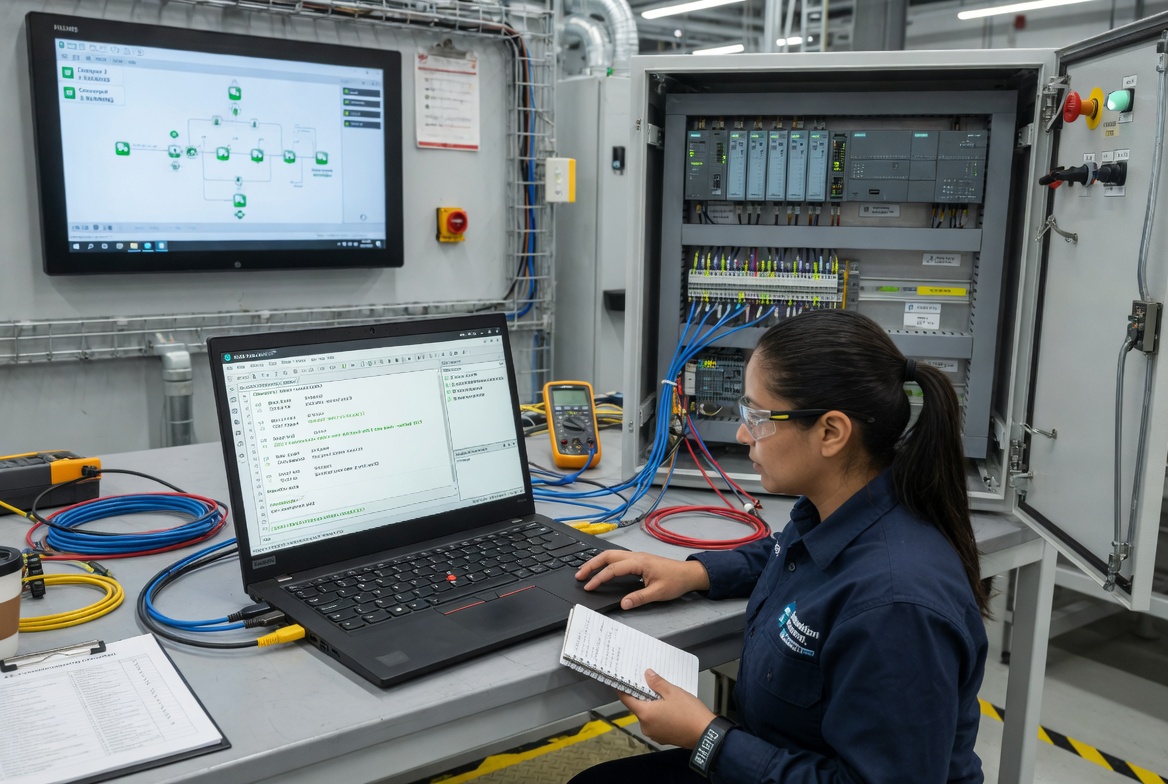
PLC Programming & Control Systems
We program control logic for pharmaceutical and medical device applications using Siemens, Mitsubishi, and Unitronics platforms. Every program is developed to meet the strict documentation and repeatability standards that validated environments require. Our approach ensures that all code is fully traceable, supporting your audit readiness from the start. We prioritize high-performance logic that maintains production consistency across every cycle.
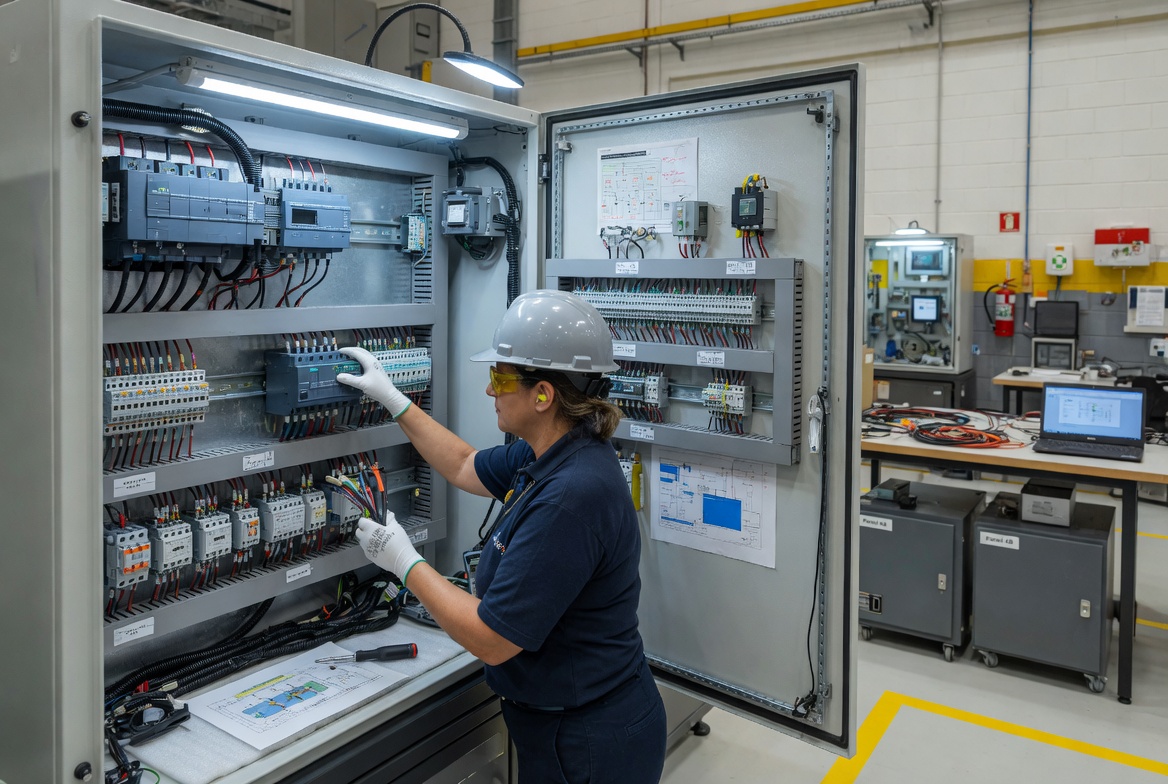
Electrical Control Panel Design & Build
We design and manufacture control panels engineered for clean room compatibility, ensuring they meet the stringent demands of your facility. Every panel is built with full documentation of all components, sourcing, and testing results to directly support your validation records. Our designs prioritize durability and compliance, providing a reliable foundation for your most critical manufacturing processes. This commitment to transparency helps streamline your validation and qualification efforts.
Systems Integration
Our team integrates SCADA, MES, and ERP systems into your existing production environment without compromising the validated state of your facility. We carefully manage every connection to ensure that new capabilities do not introduce compliance risks or data gaps. By synchronizing your disparate technologies, we create a cohesive infrastructure that supports consistent, repeatable production. This seamless integration ensures your systems work together to uphold your quality and regulatory standards.
HMI & SCADA Development
We build operator interfaces and SCADA dashboards specifically designed to maintain data integrity and strict clean room protocol compliance. These systems provide your team with clear, real time visibility into your production lines without breaking essential clean room discipline. We focus on creating intuitive controls that reduce the potential for human error while ensuring all interactions are secure and logged. This enhances operational transparency and supports your overall quality management goals.
Environmental Monitoring Systems (EMS)
We design independent environmental monitoring systems that track temperature, humidity, and pressure separately from standard building automation. This separation ensures that your critical environmental data remains secure and untainted, protecting the data integrity your quality system depends on. By providing accurate, real time monitoring, our solutions help you maintain the precise conditions required for sensitive medical and pharmaceutical processes. This proactive approach supports continuous compliance and protects your product quality.
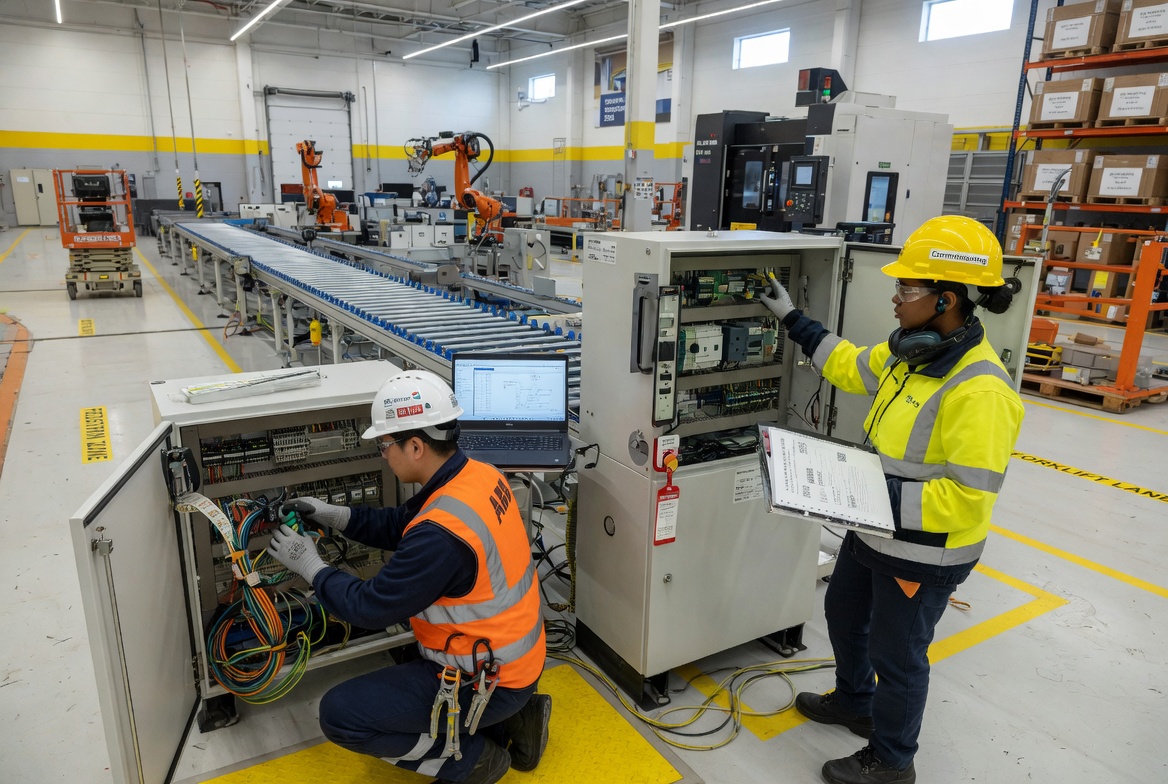
Installation & Commissioning
Our team handles all aspects of on site installation and commissioning, providing the detailed, qualification ready documentation you need for successful deployment. We support your Installation Qualification (IQ) and Operational Qualification (OQ) processes from the very beginning of the project. By managing these critical steps, we ensure that your equipment is set up to meet all regulatory and performance specifications. This thorough approach provides a solid foundation for your ongoing validation efforts.
Remote Monitoring & Telemetry
Our secure, remote monitoring solutions provide you with real time diagnostics and immediate alerts for your production lines. This technology helps you detect and address environmental or process deviations quickly, before they have the chance to threaten a batch or compromise your validation status. By bridging the gap between your on site machinery and remote oversight, we ensure your team stays informed at all times. This supports proactive management and reduces the risk of unexpected production interruptions.
Compliance, Validation
& Data Integrity
Pharmaceutical and medical device manufacturing runs on documented, defensible processes, and our systems are designed to support that from the start.
We design with FDA 21 CFR Part 11 in mind, which governs how electronic records and electronic signatures must be created, secured, and audited. In practical terms, this means every system we build supports complete audit trails, secure access control, and reliable electronic record-keeping.
We also design around GMP requirements, ensuring that any change made to a system—whether during initial commissioning or years later during an upgrade—preserves the facility's validated state rather than putting it at risk.
For batch release and fill-finish processes, we build in the precise, repeatable sequencing these processes demand, so your production consistency supports rather than complicates your quality assurance work.
FDA 21 CFR Part 11 Ready
Our SCADA and HMI solutions feature complete electronic audit trails, secure electronic signatures, and tamper-evident records to ensure effortless audit defense.
GMP & GAMP 5 Discipline
We follow Good Automated Manufacturing Practice (GAMP 5) lifecycle models, ensuring every software function and hardware modification preserves your validated state.
Tri-Certified Quality Rigor
Holding ISO 9001 (Quality), ISO 17020 (Inspection), and ISO 17025 (Calibration), MASK brings verifiable calibration and documentation rigor to medical automation.
Clean-Room Engineering
Panel and sensor architectures engineered specifically for ISO Class 5-8 clean-rooms, respecting laminar airflow patterns and aggressive sanitization regimes.
Supporting Pharmaceutical & Medical Manufacturers Worldwide
We are headquartered in Cullompton, Devon, in the United Kingdom, and we apply the same engineering discipline and validation-aware design process to pharmaceutical and medical device projects across three continents.
Whether your facility is based in the UK, mainland Europe, North America, or beyond, you receive the same rigorous process, the same certified quality management systems, and the same commitment to long-term lifecycle support.
Fast on-site engineering, commissioning support, and scheduled preventative maintenance across the UK Golden Triangle and European life science hubs.
Turnkey panel builds with full FAT documentation dispatched worldwide, accompanied by on-site IQ/OQ execution and operator training.
Encrypted remote diagnostic gateways enabling secure oversight and instant troubleshooting without breaching clean-room airlocks.
How We Work
We follow a structured, documentation-led process on every pharmaceutical and medical device project:
Consultation & Audit
We assess your user requirements (URS), clean-room classification, validation status, and project feasibility before engineering commences.
Design & FDS
Our engineers develop functional design specifications, electrical schematics, and software architectures strictly aligned with GMP and GAMP 5.
Build & In-House FAT
We manufacture clean-room panels and code logic in-house, executing rigorous Factory Acceptance Testing with complete qualification documentation.
Commissioning & IQ/OQ
We install on-site under clean-room protocols, execute formal IQ/OQ testing, and train your staff, maintaining complete audit trails throughout.
Validated Lifecycle Support
We provide ongoing preventative servicing, remote telemetry, and formal change control support to help you maintain your validated state over time.
Why Manufacturers Choose MASK for
Pharmaceutical & Medical Automation
We hold ISO 9001, ISO 17020, and ISO 17025 certifications, and we bring that same quality management discipline to every pharmaceutical and medical device project. Our team works across Siemens, Mitsubishi, Unitronics, Allen-Bradley, and Omron platforms, so we recommend the right technology for your application rather than defaulting to a single vendor's equipment.
We manage every project end to end, from initial design through build, installation, commissioning, and ongoing support, so you work with one accountable engineering partner rather than coordinating multiple contractors.
As the shortage of validation-experienced automation engineers continues to affect the sector, we act as an experienced outsourced team who already understands GMP, data integrity, and the documentation this industry demands.
Tri-Certified Quality Framework
ISO 9001, ISO 17020, and ISO 17025 certified quality management protocols applied to all panel manufacturing, software verification, and sensor calibration.
Vendor-Agnostic Objectivity
Specialist expertise across Siemens, Mitsubishi, Unitronics, Allen-Bradley, and Omron controllers. We select what best satisfies your clean-room specifications.
Single Accountable Partner
End-to-end delivery from URS translation and electrical schematics to clean-room IQ/OQ and ongoing SLA support under one roof.
Bridging the UK GAMP Skills Gap
Immediate access to senior automation engineers with deep validation pedigree, eliminating months of costly internal recruitment and training.
Frequently Asked Questions
Key questions pharmaceutical and medical device manufacturers ask when evaluating MASK Control Systems:
Does MASK have experience with GMP-validated environments?
What is FDA 21 CFR Part 11, and how does MASK design for it?
Can you automate clean-room environments without disrupting existing validation?
Do you support batch release and fill-finish processes?
Do you deliver pharmaceutical automation projects outside the UK?
Explore Other Industries We Serve
In addition to pharmaceutical and medical devices, MASK engineers bespoke control and automation systems across diverse industrial sectors:
Get In Touch With Our Validation Engineers
If you are planning a pharmaceutical or medical device automation project, or you need to modernize a validated system, our team is ready to help. Explore our other industry sectors or contact us directly to discuss your requirements.