Food & FMCG Automation Solutions
MASK Control Systems designs and delivers automation solutions for food and beverage manufacturers across the UK and worldwide. Since 2013, we have engineered PLC control systems, hygienic control panels, and full production line integrations for FMCG operations that demand speed, hygiene, and consistency at every stage.
Why Food & FMCG Production Lines Need Specialized Automation
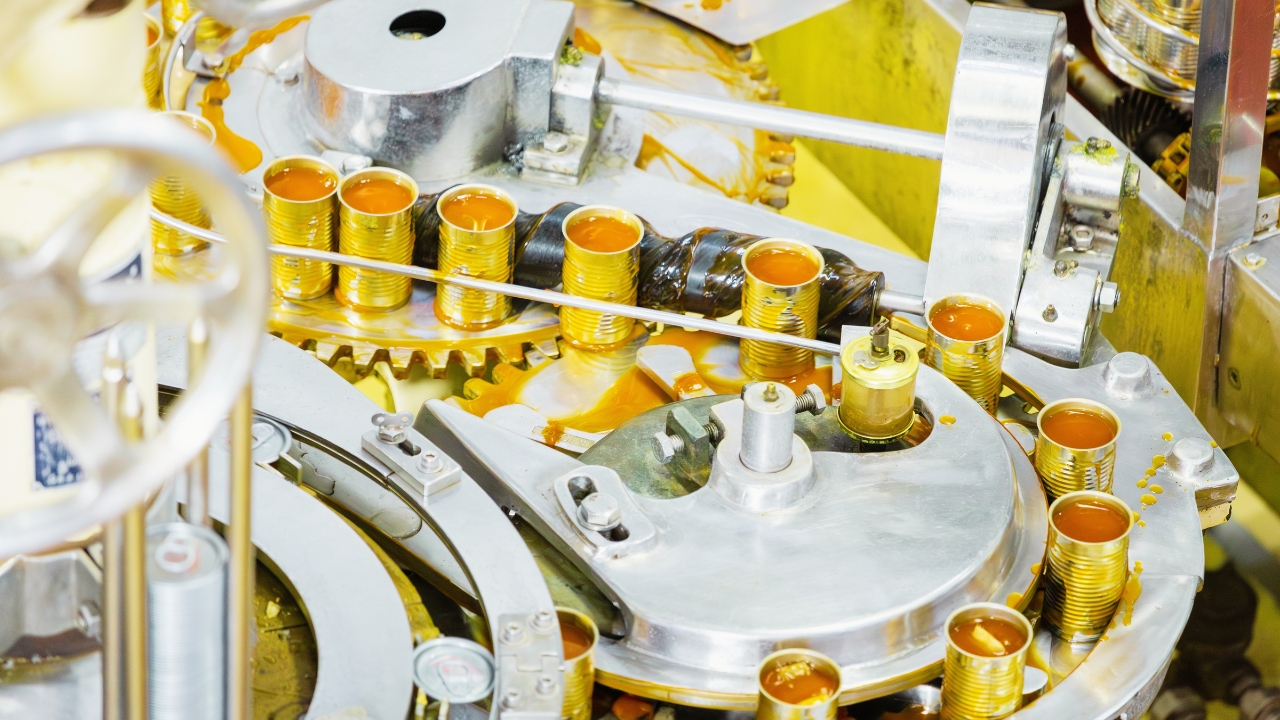
Food and FMCG production lines operate under pressures that most other industries do not face. Packaging and filling lines often run at hundreds of units per minute, and a control system must respond in milliseconds to keep pace without introducing errors.
Manufacturers also handle multiple SKUs on the same line, which means automation must support fast changeovers without long downtime or heavy operator intervention.
Hygiene adds another layer of complexity. Food-grade environments require washdown-rated equipment, contamination prevention built into the system design, and full traceability that can withstand an audit. On top of all this, every percentage point of overall equipment effectiveness (OEE) directly affects your bottom line, so reliability and fast fault recovery are not optional. We design every system with these pressures in mind from the first specification meeting.
Milliseconds Response
High-speed packaging synchronization handling hundreds of units per minute cleanly.
Rapid Recipe Switching
Touchscreen SKU changeovers reducing line conversion downtime from hours to minutes.
The Hygiene & OEE Demands
- IP66/IP69K Washdown: Cabinets and field cabling rated to withstand high-pressure, chemical caustic sanitation.
- Full Batch Traceability: Automated tracking from raw ingredient intake through to finished pallet serialization.
- Contamination Prevention: Sloped roofs, stainless hardware, and crevice-free mechanical engineering.
- OEE Revenue Gain: Every 1% improvement in availability delivers thousands in weekly profit.
The UK Food & Drink Manufacturing Landscape
Food and drink manufacturing is the largest manufacturing sector in the UK, with a combined turnover of more than £148 billion and a Gross Value Added (GVA) of £37 billion to the economy. The sector includes over 12,000 manufacturers, and the vast majority—around 97 percent—are small and medium-sized businesses rather than large multinational operations.
This scale comes with real pressure. Labor shortages in food and drink manufacturing have consistently run higher than the wider UK manufacturing average, and industry research has pointed to billions of pounds in lost output as a direct result.
At the same time, industry analysis has identified a significant untapped opportunity, worth an estimated £7 to £14 billion, that could be unlocked through greater investment in automation, digital systems, and connected production technology. For SME manufacturers, this makes automation less of a luxury and more of a practical response to a labor market that is not getting easier.

Signs Your Production Line Needs Automation
Many manufacturers reach out to us after noticing the same warning signs on their line. If any of the following sound familiar, it is worth a conversation:
End-of-Line Bottlenecks
Manual palletizing or pick-and-place tasks are creating severe bottlenecks, restricting your entire upstream plant throughput.
Lengthy SKU Changeovers
Switching between product recipes or packaging formats takes hours of mechanical adjustments and eats into productive line time.
Paper-Based Traceability Risks
Relying on manual clipboard logs and paper batch records slows down BRCGS / HACCP audits and risks human transcription errors.
Recurring Unplanned Stoppages
Intermittent sensor trips, conveyor jams, or motor overloads are becoming daily occurrences rather than rare exceptions.
Overstretched Engineering Staff
Your internal maintenance team is consumed by daily firefighting, leaving zero bandwidth to research, engineer, or deliver new automation.
Automation Skills Shortage
Struggling to recruit or retain senior PLC and control engineers with the specific platform experience required for modern lines.
Our Food & FMCG Automation Services
Comprehensive engineering disciplines built to keep your output high, changeovers rapid, and downtime minimal.

PLC Programming & Control Systems
Our PLC programming services focus on creating robust, reliable control logic tailored for food and beverage production environments. Utilizing industry-standard platforms like Mitsubishi, Siemens, and Unitronics, we engineer solutions that streamline critical operations such as filling, capping, wrapping, and checkweighing. By moving beyond isolated machine operation, we provide full line integration that ensures every component of your production process works in perfect harmony. This unified approach minimizes process bottlenecks and maximizes the consistency of your output.
Electrical Control Panel Design & Build
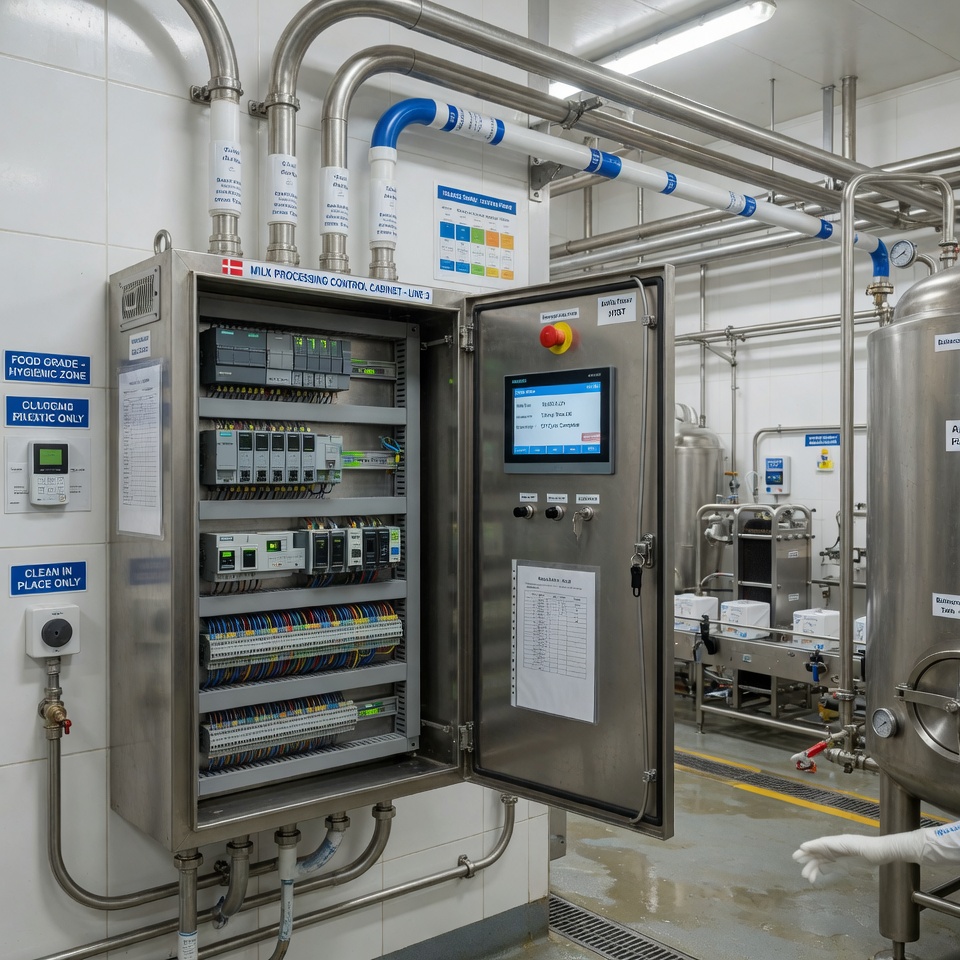
We specialize in the design and manufacture of custom electrical control panels that are engineered specifically for the harsh realities of food and beverage manufacturing. Every panel is built to meet strict hygiene requirements, ensuring durability against the rigorous washdown cycles and sanitation standards common on a busy production floor. Our design philosophy prioritizes both structural integrity and compliance, ensuring that your controls are protected from environmental hazards. By building systems that withstand these demanding conditions, we ensure long-term reliability and minimize maintenance needs for your facility.
Systems Integration & Conveyor Control
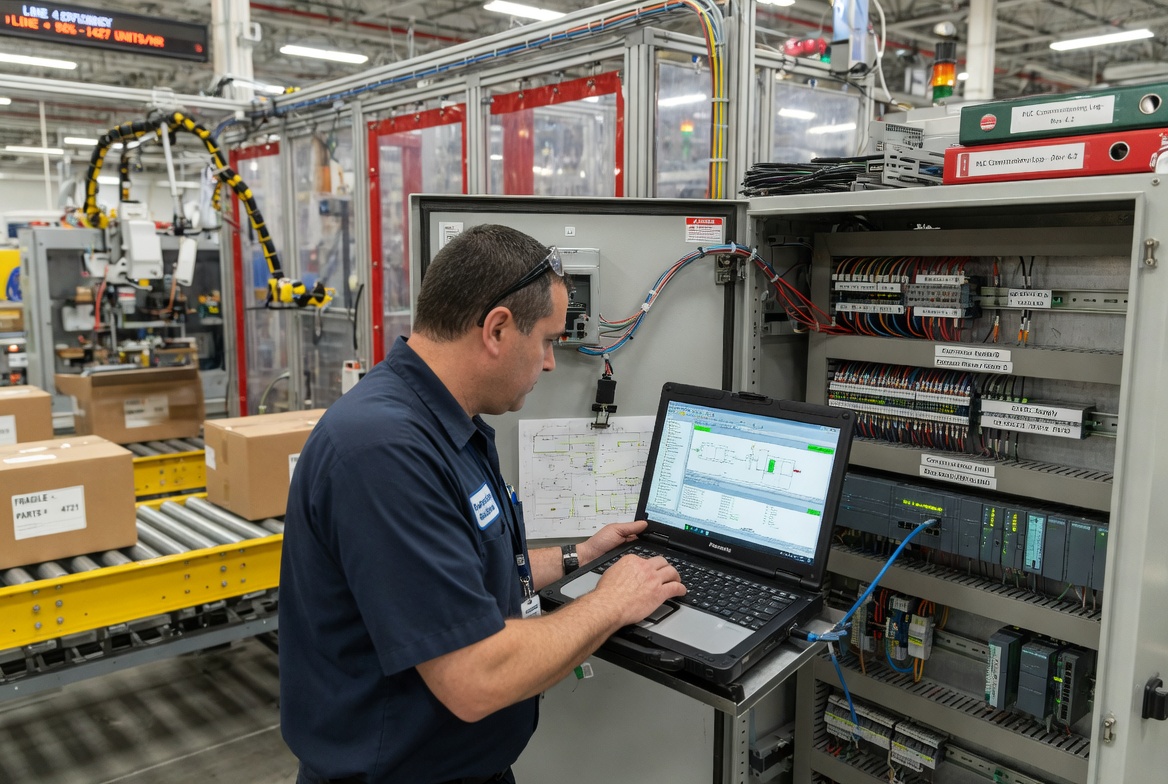
Our systems integration services focus on orchestrating smooth, efficient product flow across your entire production line. We design intelligent conveyor control systems that incorporate advanced accumulation and divert logic, ensuring that your materials move seamlessly from start to finish. Instead of allowing your machines to function as disconnected, independent units, we integrate them into a cohesive system that optimizes throughput. This comprehensive coordination reduces downtime caused by jams or mismatches, allowing for a more fluid and productive manufacturing environment.
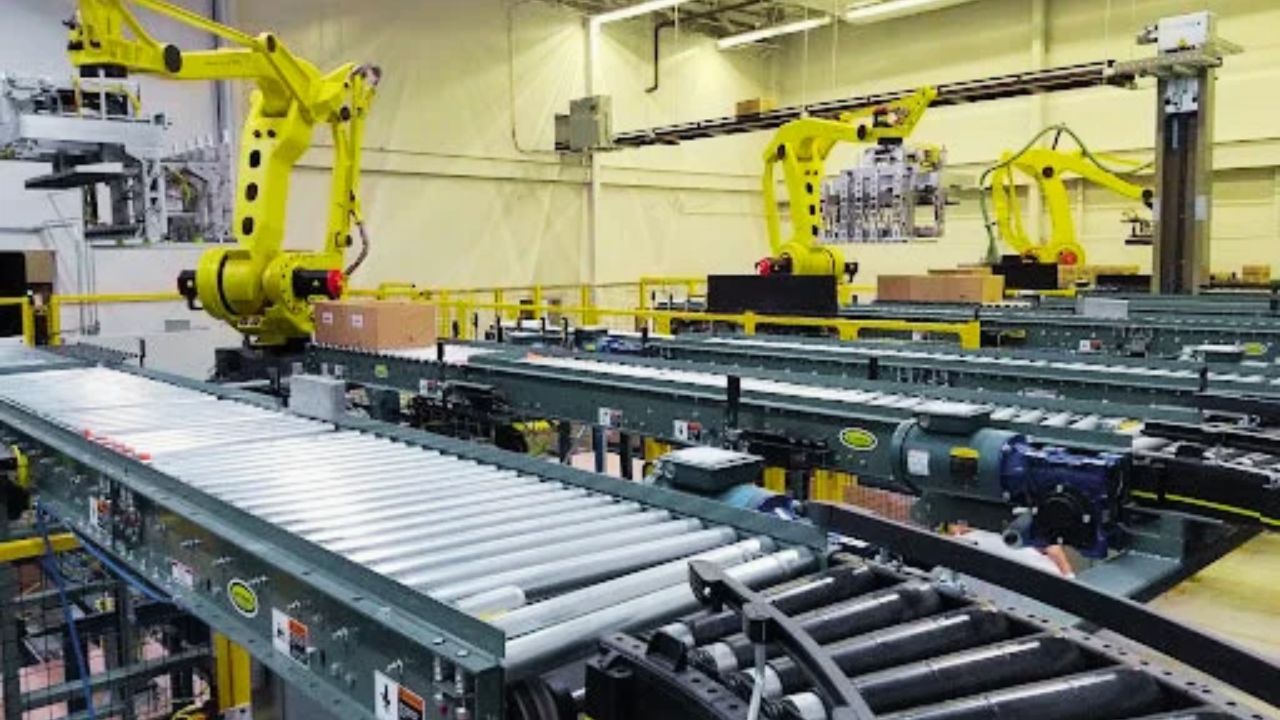
Robotic Palletizing & End-of-Line Automation
We provide end-of-line automation solutions featuring robotic palletizing cells that significantly boost consistency and throughput while removing the need for manual, repetitive lifting. Our designs address safety and space constraints by offering both fenceless and fully guarded configurations tailored to your specific floor plan and line speed requirements. By automating this final stage, we reduce the risk of workplace injuries and eliminate bottlenecks at the end of your process. This creates a more reliable workflow that keeps pace with your upstream production while maintaining high standards of quality.
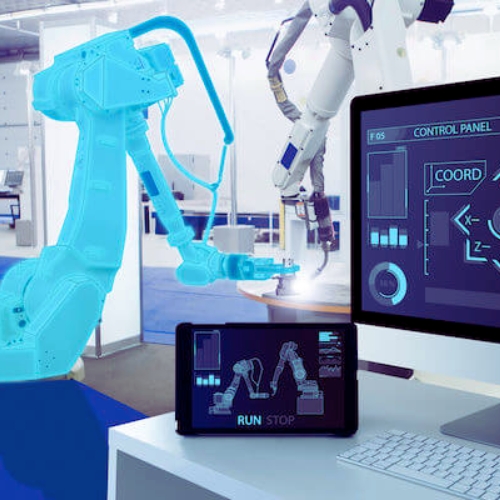
HMI & SCADA Development
Our HMI and SCADA development services provide your team with powerful, intuitive interfaces for monitoring and controlling your production environment. Designed specifically for fast-changeover environments, these dashboards offer clear visibility into real-time performance and instant control during SKU switches or production runs. We prioritize usability and data accessibility, ensuring that operators can make informed decisions quickly. By simplifying complex operational data into actionable insights, our systems empower your team to maintain efficiency even when production requirements change rapidly.
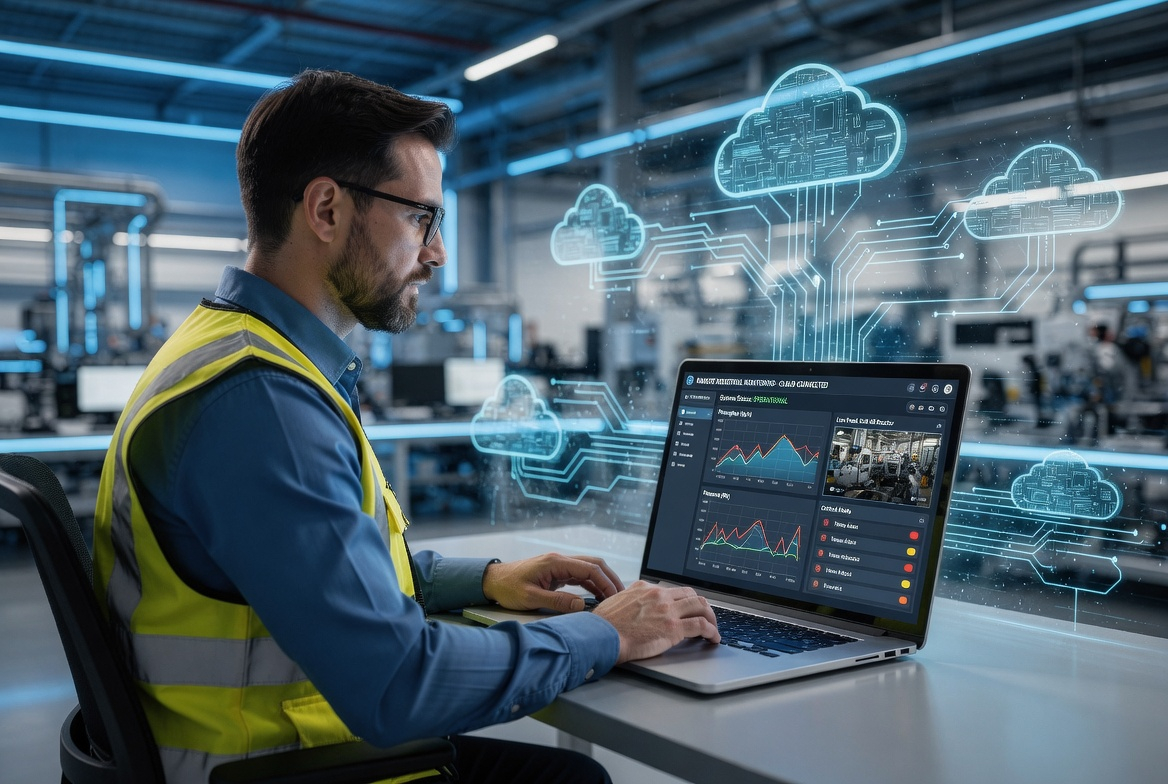
Remote Monitoring & Telemetry
We provide secure, cloud-based remote monitoring solutions that offer real-time diagnostics and proactive alerts for your production lines. Using industry-standard protocols like OPC UA, MQTT, and HTTPS, our systems provide instant visibility into your operations from any location, allowing for immediate response to potential faults. This integration bridges the critical gap between on-site machinery and off-site oversight, ensuring that performance data is always accessible for review. By identifying issues before they escalate, our monitoring approach reduces reactive repairs, lowers maintenance overhead, and creates a smarter, data-driven foundation for factory management.
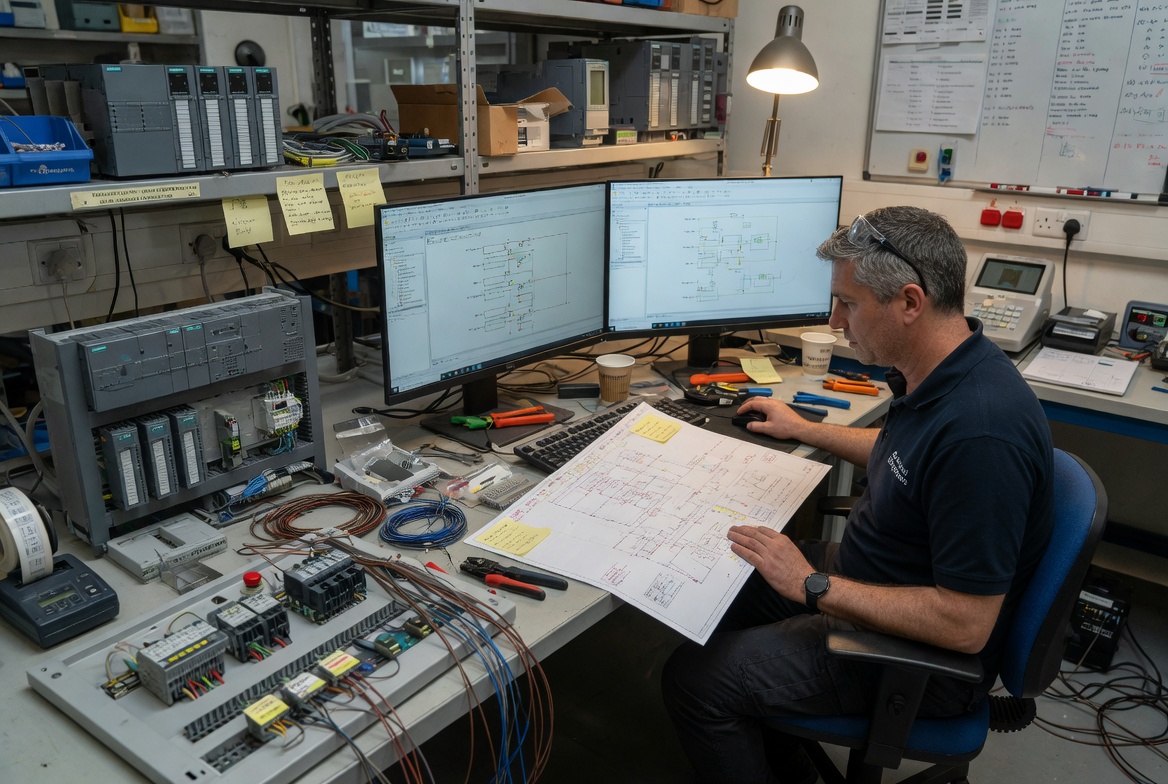
Offline Programming & Commissioning Support
Our offline programming and commissioning support services are designed to minimize your operational downtime by perfecting control logic before it is deployed. We build and thoroughly test your software in a controlled, virtual environment, allowing us to identify and resolve issues early in the process. This meticulous pre-testing phase significantly reduces the risk of installation delays and compresses the overall commissioning window. By moving the majority of the integration work off-site, we ensure a faster, more seamless transition to your production floor during final implementation.
Installation & Commissioning
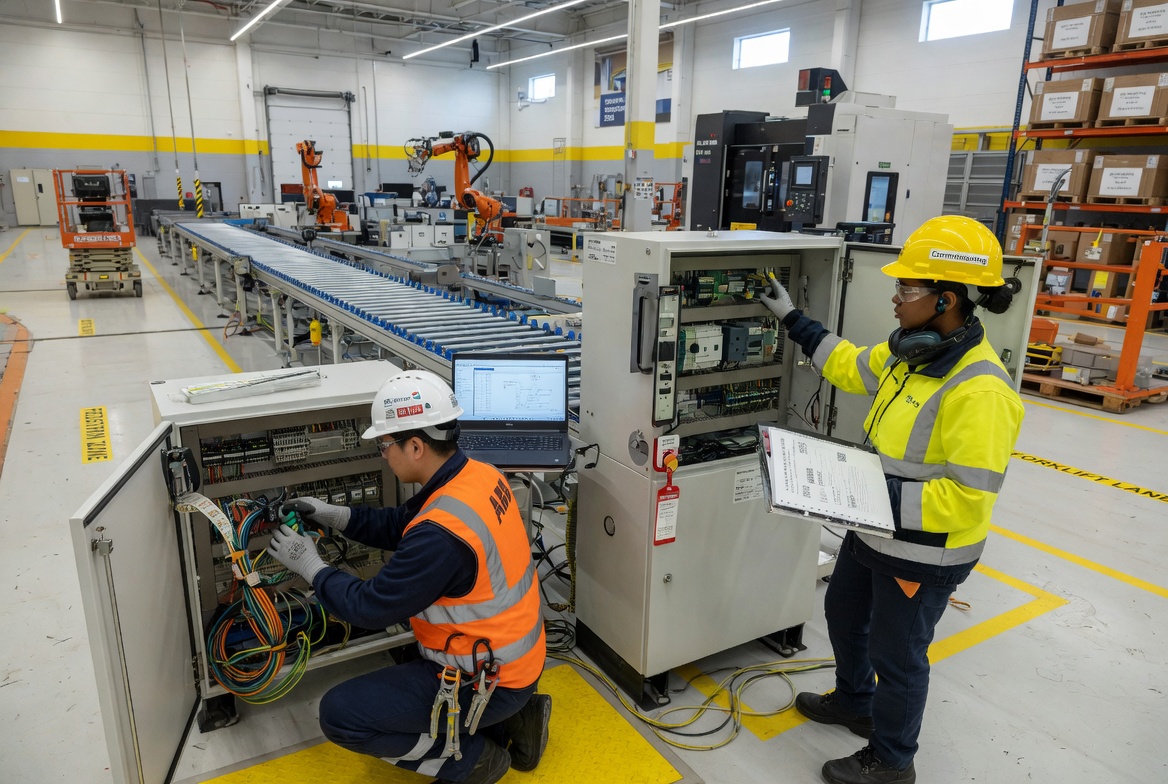
We manage your entire on-site installation and commissioning project, providing comprehensive support from initial equipment setup to final production sign-off. Our team handles every critical step, including rigorous I/O testing, dry cycling, and wet product trials, to verify that your new system performs exactly as specified. We remain actively involved throughout the entire deployment phase, ensuring that all systems are fully integrated and optimized for your unique operational requirements. Our commitment continues until a successful, full handover is achieved, giving you complete confidence in your new automation solution.
Compliance & Traceability Built In
Food and FMCG manufacturers operate under strict hygiene and quality frameworks, and we design our systems to support them rather than work around them.
Our automation solutions align with HACCP and BRCGS standards, and we build full audit traceability into every system, from ingredient intake through to the finished pallet. When your hygiene certification audit comes around, your automation system supports the process instead of complicating it.
Energy Efficiency & Operational Cost Reduction
Automation does more than increase speed. Well-designed control systems reduce energy consumption through smarter motor control, optimized cycle timing, and reduced waste from inconsistent manual processes.
For manufacturers facing rising energy costs, this is often one of the more immediate and measurable returns from an automation upgrade, alongside direct labor and downtime savings.
How We Work
Every food and FMCG project follows the same structured engineering process, regardless of scale or location.
Consultation
We review your current line, evaluate physical bottlenecks, understand recipe variables, and align on your target OEE metrics.
Design
Our engineers develop hygienic control system schematics, 3D cabinet models, and safety loop specifications tailored to your compliance needs.
Build & Test
We manufacture washdown panels and write control logic in-house, conducting comprehensive virtual simulation and FAT before dispatch.
Commissioning
We install on-site during scheduled changeover windows, execute dry cycling and wet product trials, and train operators before handover.
Support
We deliver ongoing maintenance, 24/7 emergency response, remote telemetry oversight, and scheduled service agreements.
Why Food & FMCG Manufacturers Choose MASK
We hold ISO 9001, ISO 17020, and ISO 17025 certifications, and we apply that same level of quality management to every food and FMCG project we take on.
Our team works across Siemens, Mitsubishi, Unitronics, Allen-Bradley, and Omron platforms, so we recommend the right technology for your line rather than pushing a single vendor's equipment.
We manage every project end to end, from initial design through build, installation, commissioning, and ongoing 24/7 breakdown support, so you work with one accountable partner rather than juggling multiple contractors. As recruiting in-house automation engineers becomes harder across the industry, we act as an experienced outsourced engineering team that already understands the demands of food and FMCG production.
Engineering excellence dispatched nationwide and internationally across 3 continents.
One partner from concept CAD design through to final production sign-off.
Frequently Asked Questions
Clear answers regarding timelines, line retrofits, and global deployment capability.
How long does a typical food or FMCG automation project take?
Timelines depend on scope, but most projects move from consultation to commissioning within a few months. Offline virtual testing and comprehensive Factory Acceptance Testing (FAT) before installation help keep on-site downtime to an absolute minimum.
Can you upgrade an existing line instead of replacing it entirely?
Yes. Many of our projects involve integrating new automation into an existing line rather than a full rebuild, which keeps capital expenditure down and minimizes disruption to your active production schedules.
Do you work with manufacturers outside the UK?
Yes. While we are headquartered in Cullompton, Devon, in the United Kingdom, we deliver food and FMCG automation projects for manufacturers across multiple continents, applying the same rigorous engineering standards wherever your project is located.
Ready to Upgrade Your Food & FMCG Production Line?
If you are planning a new food or FMCG automation project, or you need to modernize an existing line, our team is ready to help. Contact us directly to discuss your requirements.